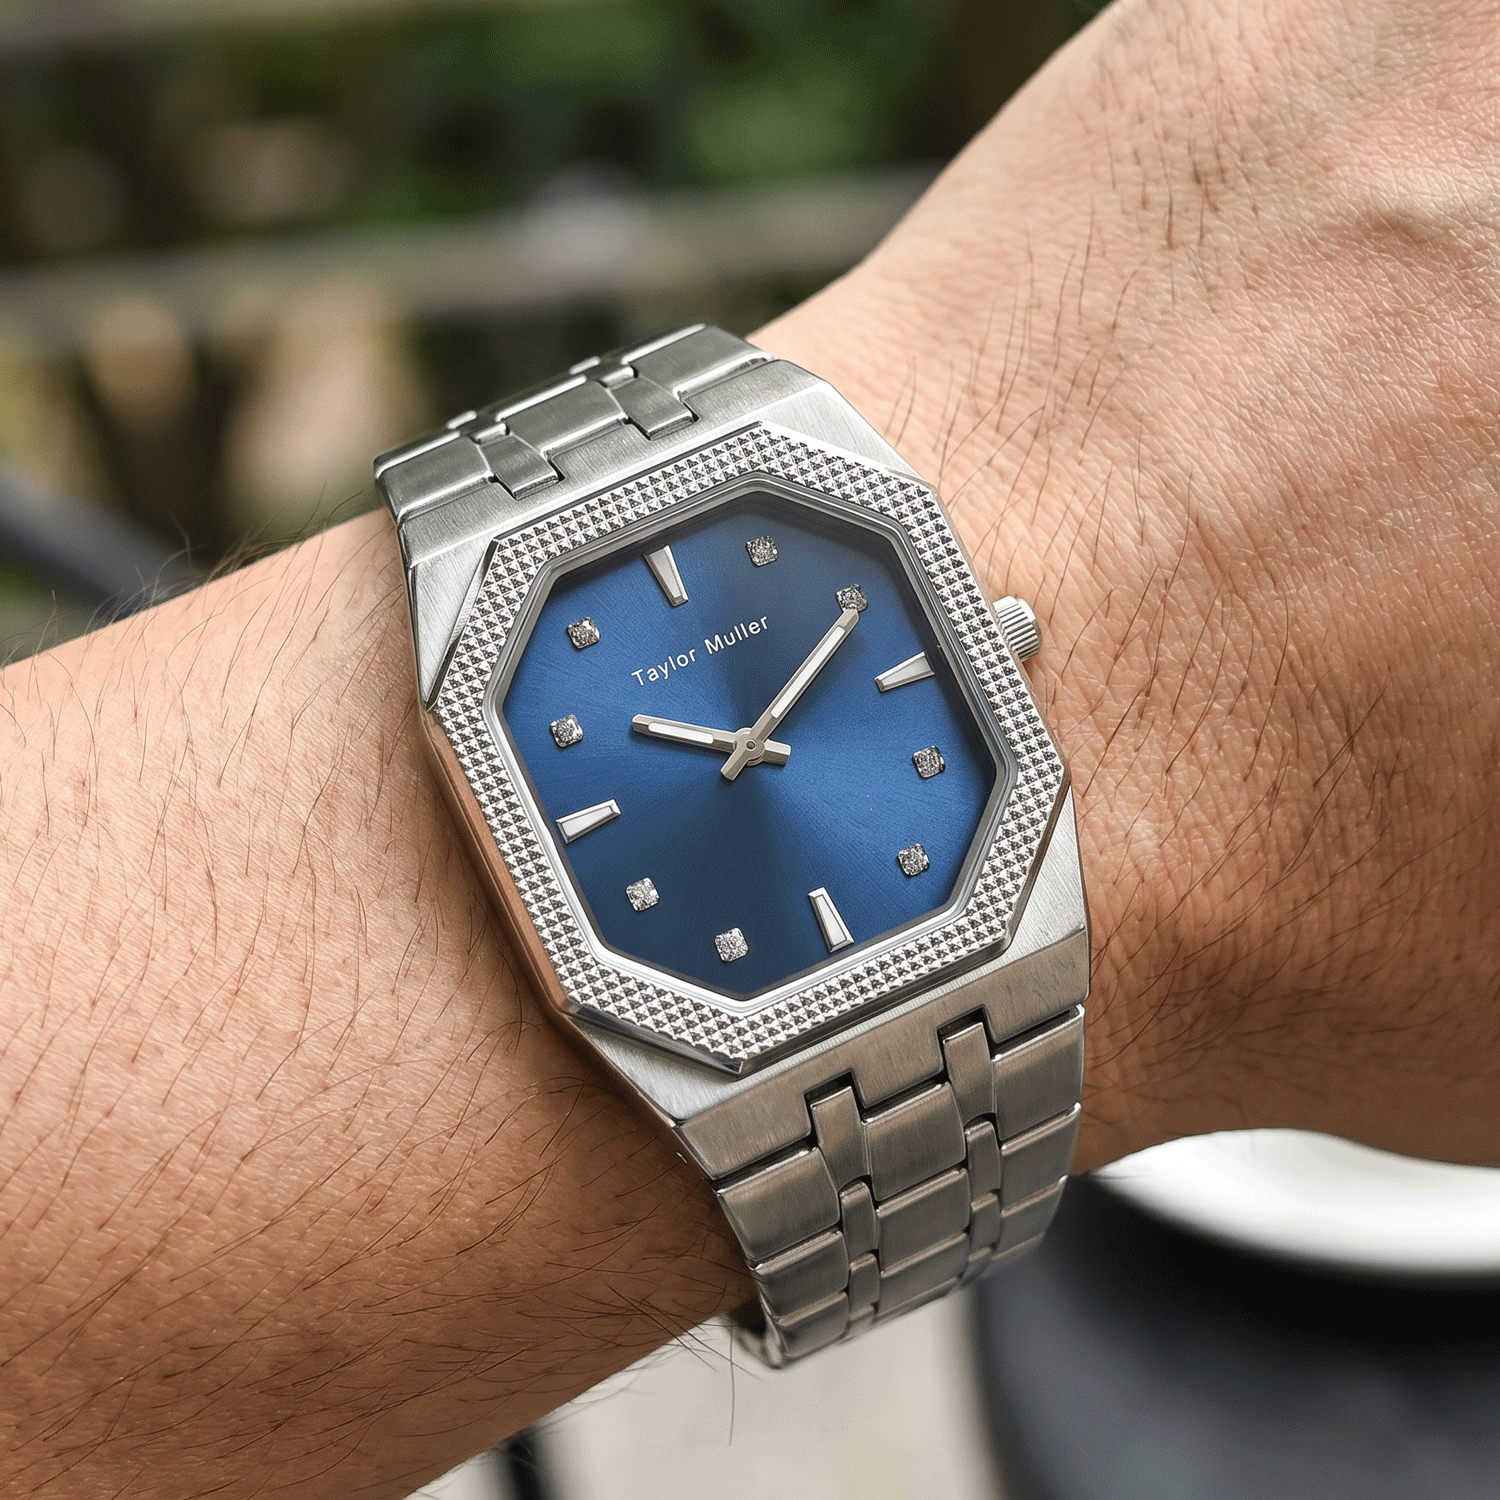

Ask a buyer to describe a watch from memory and they will describe the case: the shape, the shine, the weight on the wrist. It is also the part we make ourselves, which changes the conversation — the material is not something we order from a catalogue, it is a machining and finishing decision taken before tooling. Which is why it is worth settling before the drawing, not after the sample.
The four materials, side by side
Have a quantity in mind?
Tell us the model, the colours and the quantity — we come back with the exact MOQ, target price and lead time for your build, within 24 hours on working days.
| Material | What it is | Price position | How it finishes | What to watch |
|---|---|---|---|---|
| 304 stainless steel | The workhorse: solid stainless, machined and finished | Standard | Polished, brushed, two-tone | Nickel content — if a buyer asks for “nickel-free”, this is the conversation |
| 316L stainless steel | The marine grade, more corrosion resistance | Higher than 304 | Same range as 304 | Cost; the honest answer for salt-water markets |
| Zinc alloy | Die-cast, then plated | Lowest | Always plated: IP, PVD | Plating wears through, the watch feels light, a deep scratch shows the base metal |
| Titanium | The lightest option, and hypoallergenic | Highest | Mostly brushed or matte; mirror polishing is harder | Different wrist feel, and buyers either love it or want steel |
What actually moves the price
- The material itself. Alloy is the cheapest route, 316L costs more than 304, titanium costs the most of the four.
- How the case is formed. Stainless and titanium are cut from solid stock; alloy is cast. Two different production lines, two different tolerances.
- The finishing that follows. Plating a casting and polishing a machined case are not interchangeable — and they fail in different ways.
- Weight. It is a cost and a sales argument at once: buyers judge a watch by the wrist before they read the specification.
Matching the material to the market
Entry price points and promotional lines live comfortably in alloy: the case costs the least, and the plating gives you the colour you want. A mainstream B2B range is usually 304 — it takes a polish, it takes a brush, and it does not need plating to look finished. If the watch is sold into salt-water markets, or the buyer makes corrosion part of the pitch, 316L is the defensible answer. Titanium is for the buyer who wants light and hypoallergenic, and who is willing to pay for it. If a buyer needs a nickel-free claim, settle early which grade and which plating you are using — the claim has to hold for the whole watch, not just the case.
From our workshop
We make cases in-house, on our own tooling: stainless steel, alloy or titanium, any style, 20–60 mm or built to your size. That is why the material has to be agreed before the drawing is finalised — changing it later means new drawings and new tooling, and the sample you approved stops being the sample. It is also why we can tell you honestly what each option costs you in finishing time, rather than quoting a grade we would have to buy in. Every finished unit still goes through a water-resistance test before packing, whichever material the case is made from.
What to put in the specification
Name the grade, the size, the finish and — for alloy — the plating: for example “316L, 40 mm, brushed with polished bezel” or “zinc alloy, 38 mm, IP gold”. Add whether the case back is solid, engraved or sapphire, because that changes the assembly as well. The four manufacturing routes are on our OEM & ODM services page; the 29 references in the catalogue show how these choices look in a finished watch, and the factory page covers what we make in-house.
Send the target price, the market and the quantity per model, and we will come back with the material that fits — or tell you why the one you asked for will not hit the price. A sample runs 15–20 days and its fee comes off the bulk invoice; production is 30–45 days after approval; MOQ is 300 pcs per model, or 200 pcs when only the dial logo changes on an existing reference.
Further reading: Polished, brushed or two-tone: what case finishing really costs · Quartz or automatic, Japanese or Swiss: how to choose a movement